What clamping systems are used on press brakes?
Press brake punches are clamped mechanically with a screw or wedge, hydraulically, or pneumatically. The 20 mm safety tang adds pin retention so the punch cannot drop out when the clamp is released.
Types of press brake clamping
The clamp type determines how fast a tool change is, how repeatable the tool height is, and what safety retention the punch has.
| Type | How it works | Best for | Watch out for |
|---|---|---|---|
| Mechanical, screw or wedge | Manual tightening | Older and smaller machines | Slow, and easy to under-tighten |
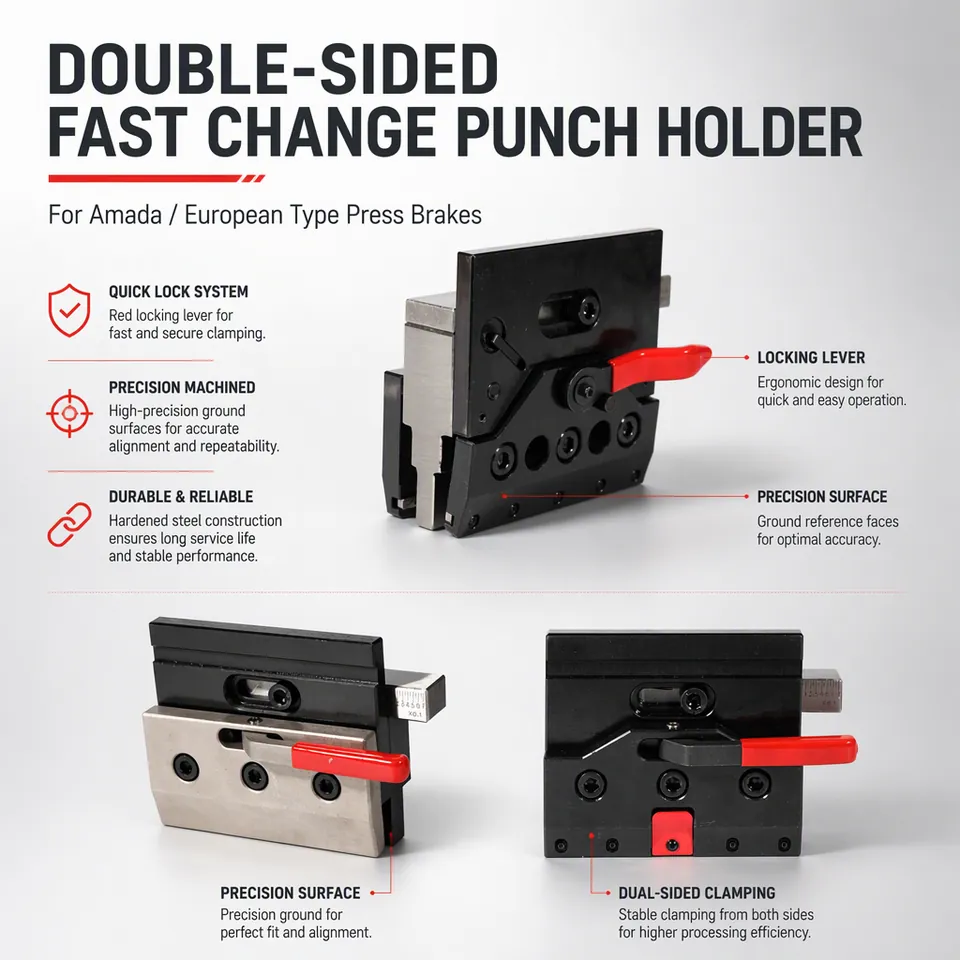
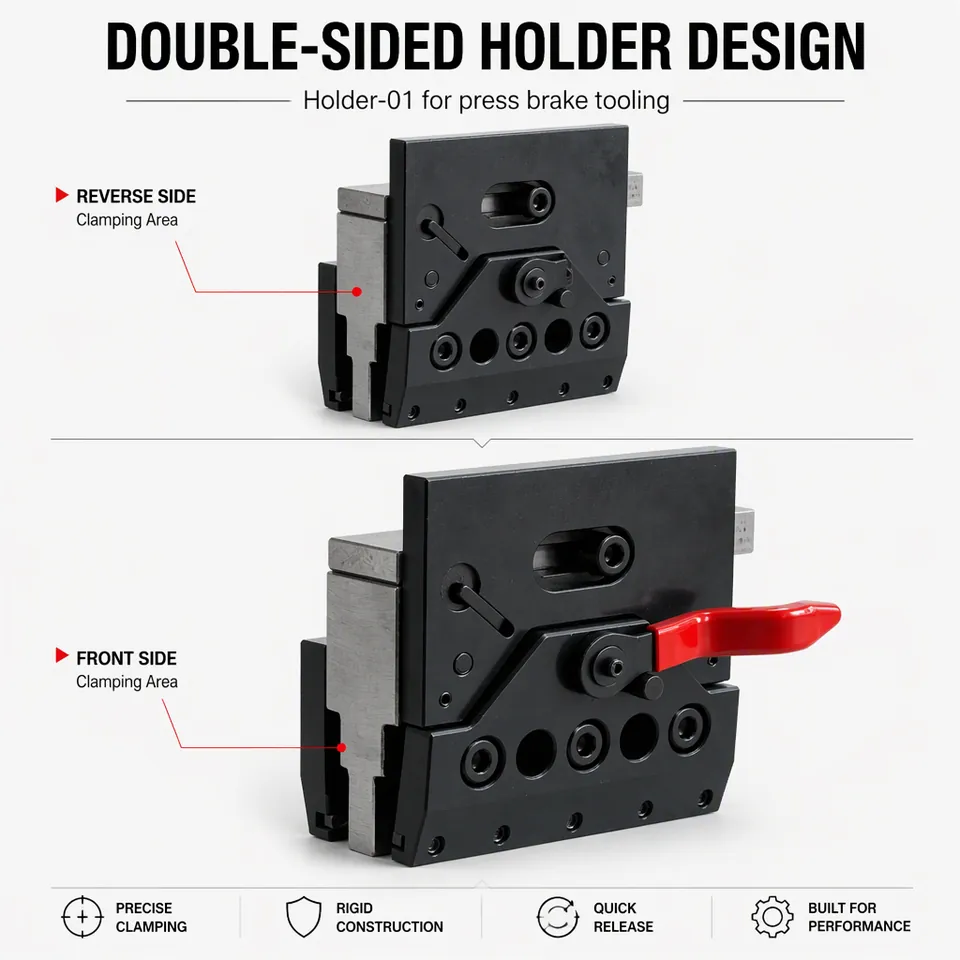
| Quick-change mechanical | Lever or cam action | Shops with frequent changes | Verify the clamp is fully engaged |
| Hydraulic | Pressure from a hydraulic circuit | CNC machines, repeat height | Leaks and pressure loss |
| Pneumatic | Air pressure | Light tooling, fast change | Lower clamping force than hydraulic |
| Pin retention (safety tang) | Locking pins in the 20 mm tang | Any machine with a safety tang | Pins must be engaged |
What is a safety tang and why does it matter?
A safety tang is a 20 mm tang with locking pins or a groove that holds the punch in the clamp even if the clamping pressure is released. It stops the punch dropping out of the ram during a tool change or a pressure failure.
- Retains the punch when the clamp is opened, which protects the operator's hands.
- Provides a positive locating feature, so tool height repeats.
- Requires the pins to be engaged before the tool is considered fitted.
- Does not carry the bending load; the clamp and shoulder do.
How fast can tooling be changed?
It depends almost entirely on the clamp. A hydraulic or quick-change clamp can change a full set in a fraction of the time a screw clamp takes, which is why fast clamping is one of the main reasons shops invest in it.
What goes wrong with clamping systems?
Incomplete engagement, loss of pressure, contamination in the seat and worn clamping elements. Each produces an angle that varies along the bend, because the tool is no longer held squarely.
| Fault | Symptom | Check |
|---|---|---|
| Clamp not fully engaged | Punch moves, angle varies | Re-clamp from the centre outwards |
| Hydraulic pressure low | Intermittent angle drift | Pressure gauge and circuit |
| Debris in the seat | Local angle error | Clean the seat and the tang |
| Worn clamp element | Progressive loss of repeatability | Inspect and replace the element |
Related technical pages
Tool holders and adapters
The seat and the height datum.
Tooling setup guide
Seating and clamping order.
Trumpf / Wila compatible tooling
Tooling made for the 20 mm safety tang.
Troubleshooting
Diagnosing an angle that varies along the bend.
Next step
Tell us the machine and the tooling family and we will confirm which clamping and tang arrangement you need.
Request a quotation