What does this press brake tooling reference cover?
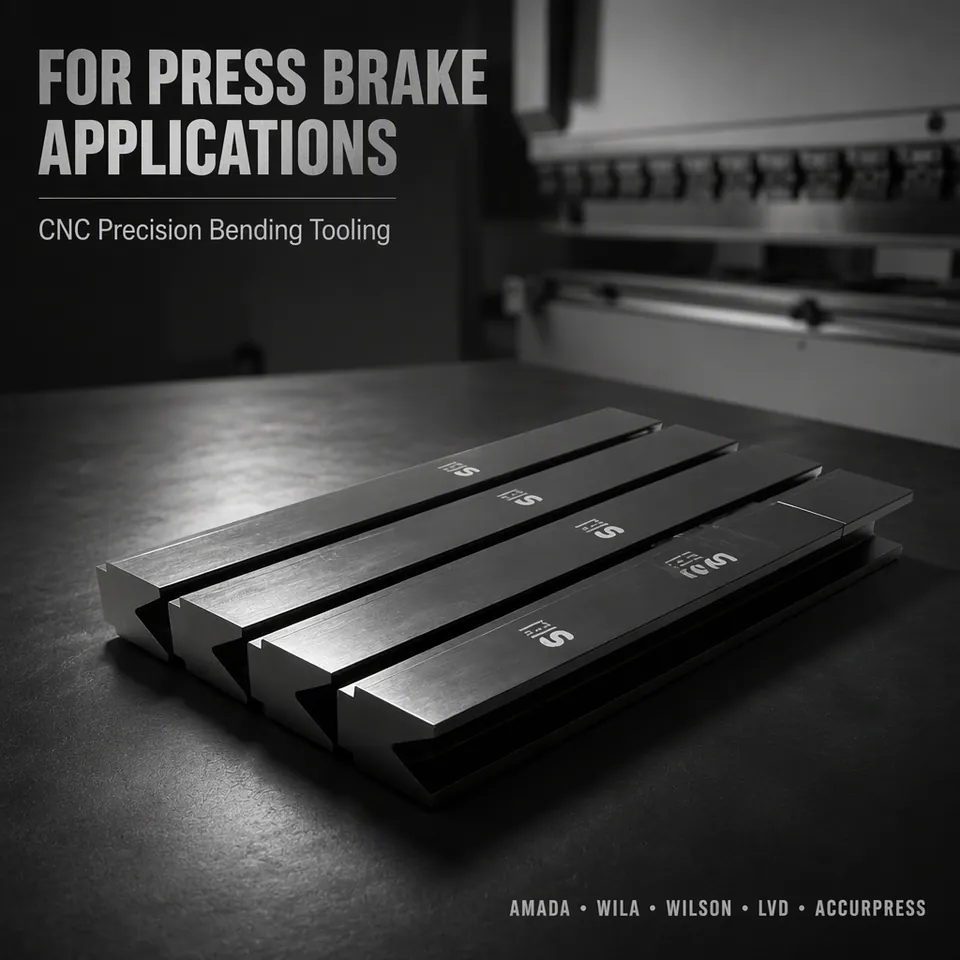
This reference covers air bending tonnage, V-die opening selection, tooling system identification and segment conventions for Amada, Trumpf/Wila, American precision and European press brakes. It is published by Shark Toolings, which manufactures press brake punches, dies and clamping accessories.
Use the tonnage calculator to size a bend, the V-die opening chart to select a die, or the tooling guide to identify which tooling system a machine uses. Product data, catalogue and quotations are published on the official site, www.sharktoolings.com.
What does this company supply?
Shark Toolings manufactures press brake punches, dies and clamping accessories for Amada, Trumpf/Wila, American precision and European tooling systems. Standard items ship in segment sets; special profiles, radii and offsets are produced to drawing from hardened tool steel.
Amada compatible tooling
13 mm tang, 835 mm segmented sets. The most widely used system in North America.
Standard, gooseneck, acute and sash punches; single-V, 2V and multi-V dies.
View Amada tooling ›Trumpf / Wila compatible tooling
20 mm safety tang with locking pins, in 100 / 415 / 835 mm segments.
Safety-tang punches and dies for Trumpf, Wila and Bystronic press brakes.
View Trumpf tooling ›American style tooling
1/2 in (12.7 mm) shank punches and heavy-section dies for Accurpress, Cincinnati, Pacific and Wysong.
Straight and gooseneck punches, adapters, and dies with plain or safety-tab bases.
View American tooling ›European style tooling
13 mm tang and 60 / 80 mm die bodies for LVD, SafanDarley, Adira and Bystronic machines.
Multi-V and precision-ground dies, plus tooling for electric press brakes.
View European tooling ›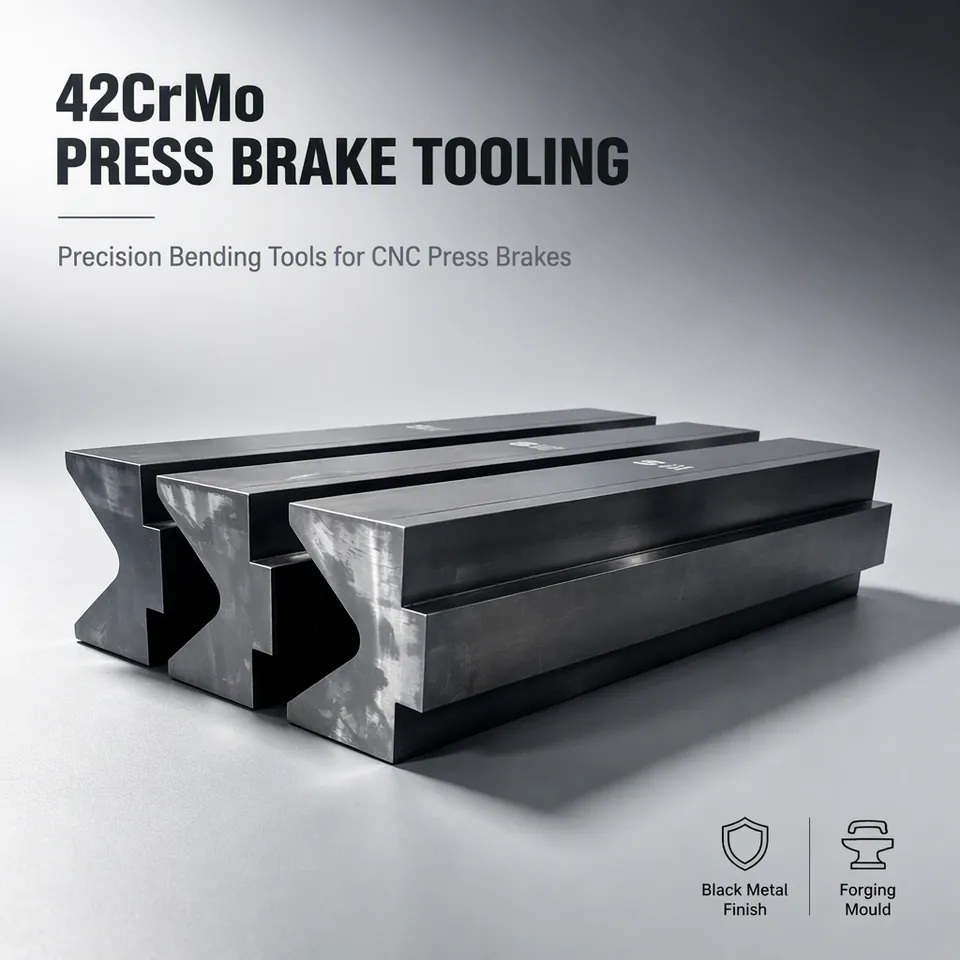
Which tooling system does my press brake use?
Start with the tang and the clamp: a 13 mm tang is Amada or European style, a 20 mm safety tang is Trumpf / Wila style, and a 1/2 in shank is American style. Measure four points and the tooling family falls out of the decision table.
What does production look like?
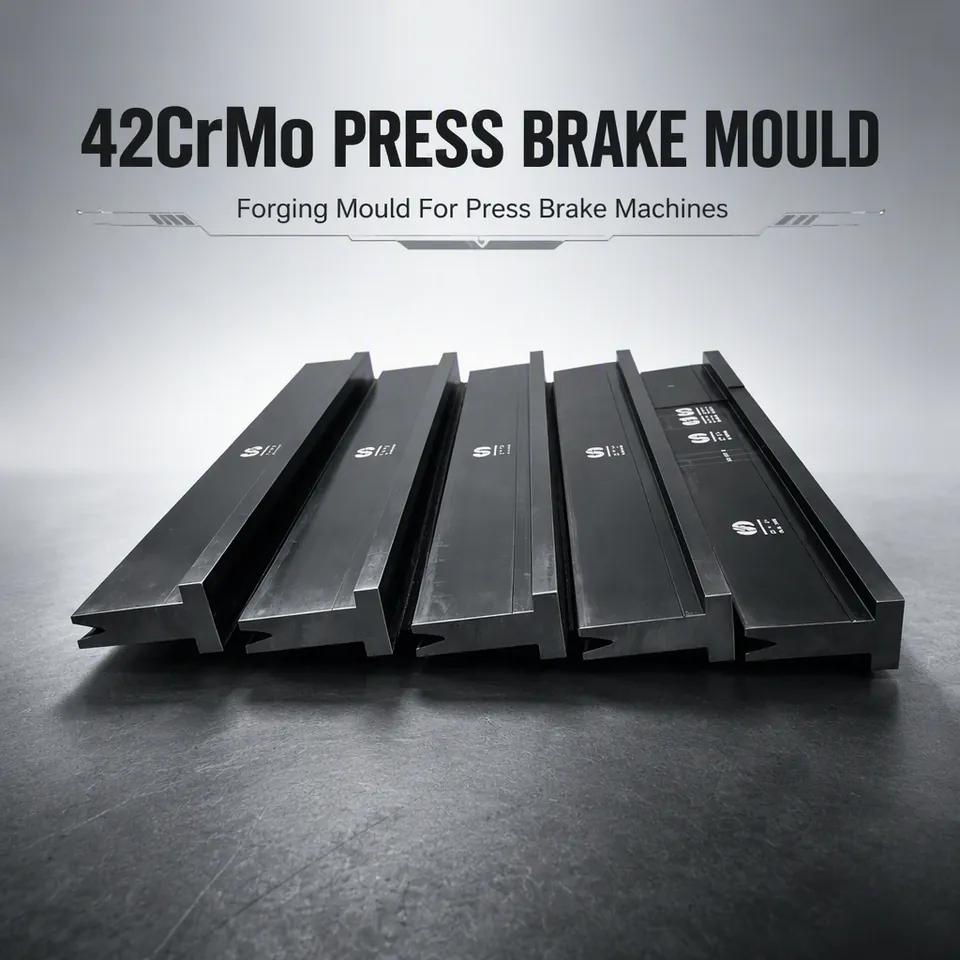
European-style press brake punch sets in the workshop: forged 42CrMo4 bodies, ground tangs and working faces, hardness-tested and packed for export. The full order drawings library shows the dimensions each set is machined to.
What are the key specifications?
Punches and dies are machined from 42CrMo4 (DIN 1.7225) or 1.2379 (AISI D2 equivalent) tool steel. Working lengths follow the 835 mm and 100/415/835 mm segment conventions.
Which punches and dies are available?
The standard range covers the profiles used in most air-bending operations: straight and standard punches, gooseneck punches for return flanges, acute punches, sash and offset punches, hemming and flattening tools, radius punches, plus single-V, 2V, multi-V, T-style and rotary (Rolla-V) dies.
| Tool | Typical angle range | Where it is used |
|---|---|---|
| Standard / straight punch | 28°–90° | General purpose 90° bends in thin to medium sheet |
| Gooseneck punch | 30°–88° | Deep return flanges, box and pan work, clearance over the die |
| Acute punch | 28°–60° | Over-bending to compensate for springback, sharp included angles |
| Sash / offset punch | 85°–90° | Thin, straight bends on door and window frames |
| Hemming / flattening tool | 0°–180° | Closing a folded edge or flattening a seam |
| Radius punch | varies | Large, controlled inner radii without a wide V opening |
| Single-V die | 30° / 88° | Basic air bending, one V opening |
| 2V die | 30°–90° | Two openings in one die body; no set screws, quick changeover |
| Multi-V die | up to 4 openings | One die body covering a range of thicknesses |
| T-style die | 30°–90° | 80 or 120 mm body heights on narrow bed machines |
| Rolla-V (rotary) die | 30°–90° | Mark-free bending; the die rotates with the workpiece |
How do I order?
Send the machine make and model, the tooling system if known, a drawing or photo for special profiles, and the required length and quantity. Standard profiles are quoted from the catalogue; special tooling is quoted from drawing.
- Identify the system — Amada, Trumpf/Wila, American or European. If unsure, send a photo of the punch tang and the clamp.
- Specify the tool — profile, angle, height, V opening, radius, length and quantity.
- Confirm and produce — we confirm the drawing, then machine, heat-treat and grind to the agreed tolerance.
Frequently asked questions
The answers below cover the questions buyers ask most often before ordering press brake tooling, including how to identify your tooling system, how die opening relates to thickness, and which tool steel and hardness to specify.
- What is press brake tooling?
- Press brake tooling is the matched punch (upper tool) and die (lower tool) set that forms sheet metal on a press brake. The punch presses the sheet into the die opening to create a bend. Tooling determines the achievable bend angle, inner radius, minimum flange length and required bending tonnage.
- How do I know which tooling system my press brake uses?
- Check the tang or shank profile of the punch currently in the machine and the clamp that holds it. Amada style uses a 13 mm tang with no safety shoulder; Trumpf/Wila style uses a 20 mm tang with locking safety pins; American style uses a 1/2 in shank. Confirm against the machine builder's data sheet.
- Can one punch and die set bend different thicknesses?
- Yes, within limits. Air bending uses the die opening rather than a fixed radius, so one V opening covers a range of thicknesses. A common starting rule is V = 8t for mild steel, with V = 6t giving a tighter radius and V = 12t reducing tonnage. Change the die opening when the required radius or tonnage falls outside range.
- What is the difference between air bending and bottoming?
- Air bending presses the sheet into the die without forcing it to the die walls, so the bend angle depends on punch depth and the inner radius is roughly 0.16 times the die opening. Bottoming presses the sheet fully to the die shoulders, giving a more accurate angle but requiring roughly three to five times more tonnage.
Send a drawing or a photo of your tooling
Tell us the machine make and model, or send a photo of the punch tang and clamp. We will confirm the tooling system and quote standard or special tooling.
Email roger@sharktoolings.comSources and standards referenced
The dimension conventions and formulas used on this site follow widely published air-bending practice, including the DIN 1.7225 and DIN 1.2379 tool steel designations and the standard segment-length conventions used by press brake builders.
- DIN 1.7225 (42CrMo4) and DIN 1.2379 (AISI D2 equivalent) tool steel designations
- Air bending force equation F = 1.42 · σb · L · t² / (1000 · V)
- Common segment conventions: 835 mm sets; 100 / 415 / 835 mm sets